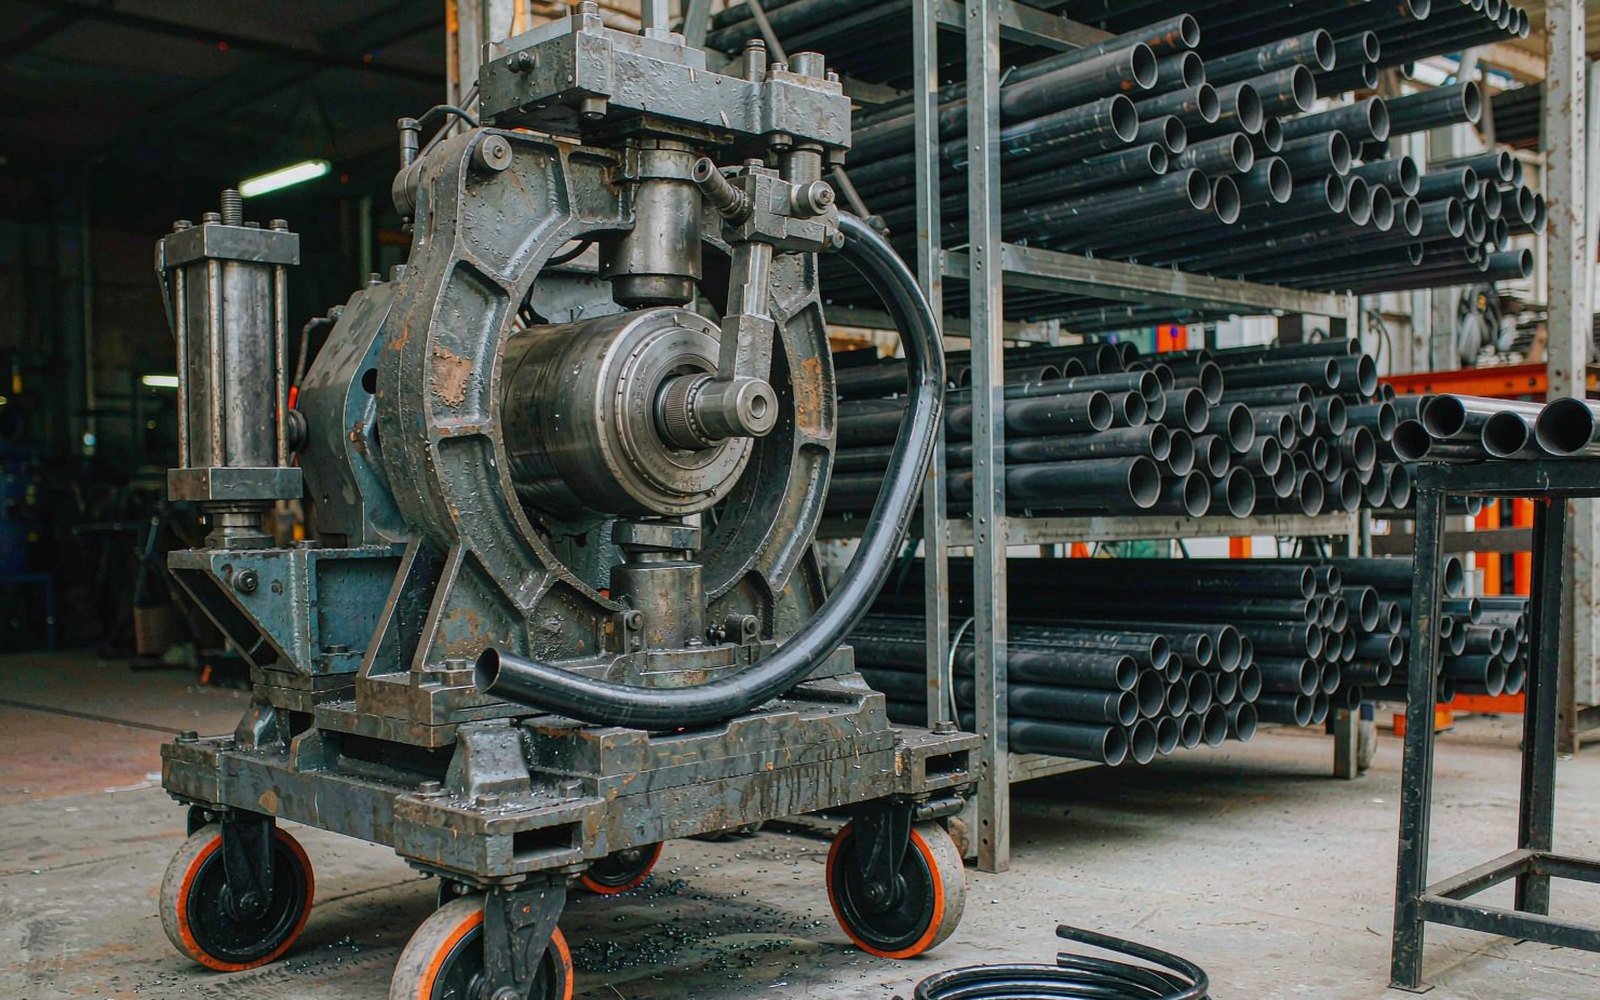
Eight processes, one roof, one team.
Nothing on our range is bought in finished. Tube is cut, bent, welded, drilled and coated, then netted, assembled and packed by the same team in Shenzhen — which is why a size change or a logo change is a working day, not a new supplier conversation.
One place to change, one place to be accountable.
The reason buyers move a steel-frame range to us is rarely the unit price on its own. It is that the frame, the net that hangs on it and the carton it ships in are made by people who sit in the same building, so a problem is fixed at the source instead of being passed between three suppliers.
- Frame and net are matched before dispatch. The net is cut and bound against the frame it will actually hang on, not to a nominal size.
- A late change stays cheap. Altering a joint, a base or a coat colour does not restart a supplier negotiation.
- One answer on lead time. No waiting on a third party to confirm whether the tube, the net or the carton is the bottleneck.
- Sampling is fast. A pre-production sample is built on the same line that will run the order.
From raw tube to sealed carton.
Every step below is carried out by our own team. What each step means for your order is listed alongside it, because that is usually the question behind the question.
| Process | What happens | What it means for your order |
|---|---|---|
| Tube cutting | Tube is cut to length on a saw and deburred before it moves on. | Frame lengths follow the drawing rather than a stock size, so a non-standard span does not need a new mould or a compromise. |
| Tube bending | Bends are formed to the drawing radius on a hydraulic bender. | Corner radius and hoop shape can be adjusted per market without re-tooling the whole frame. |
| Welding & frame assembly | Frames are welded, squared and cleaned before coating. | A weld or bracing change is a line change, not a new item — and frames are checked for square before they are coated. |
| Drilling | Fixing holes, net attachment points and base holes are drilled on the assembled frame. | Hole positions follow your net and base configuration, so aftermarket parts still line up. |
| Powder coating | Frames are coated to a RAL colour or to your sample, in matte or satin. | Your brand colour can be matched across families instead of being limited to a stock palette. |
| Netting production | Netting is produced in house to the twine and mesh specified for the item. | Net grade can be raised or lowered per market — a club-grade net and a garden-grade net are a specification choice, not a different product. |
| Net cutting & binding | Panels are cut to the frame they belong to and bound on the edge. | Panels arrive the right size, with the binding and reinforcement where the frame loads them. |
| Moulded parts | Caps, feet, joints and target panels are moulded in the same plant. | Replacement parts stay available years after the order, and a joint or foot design can be revised for your market. |
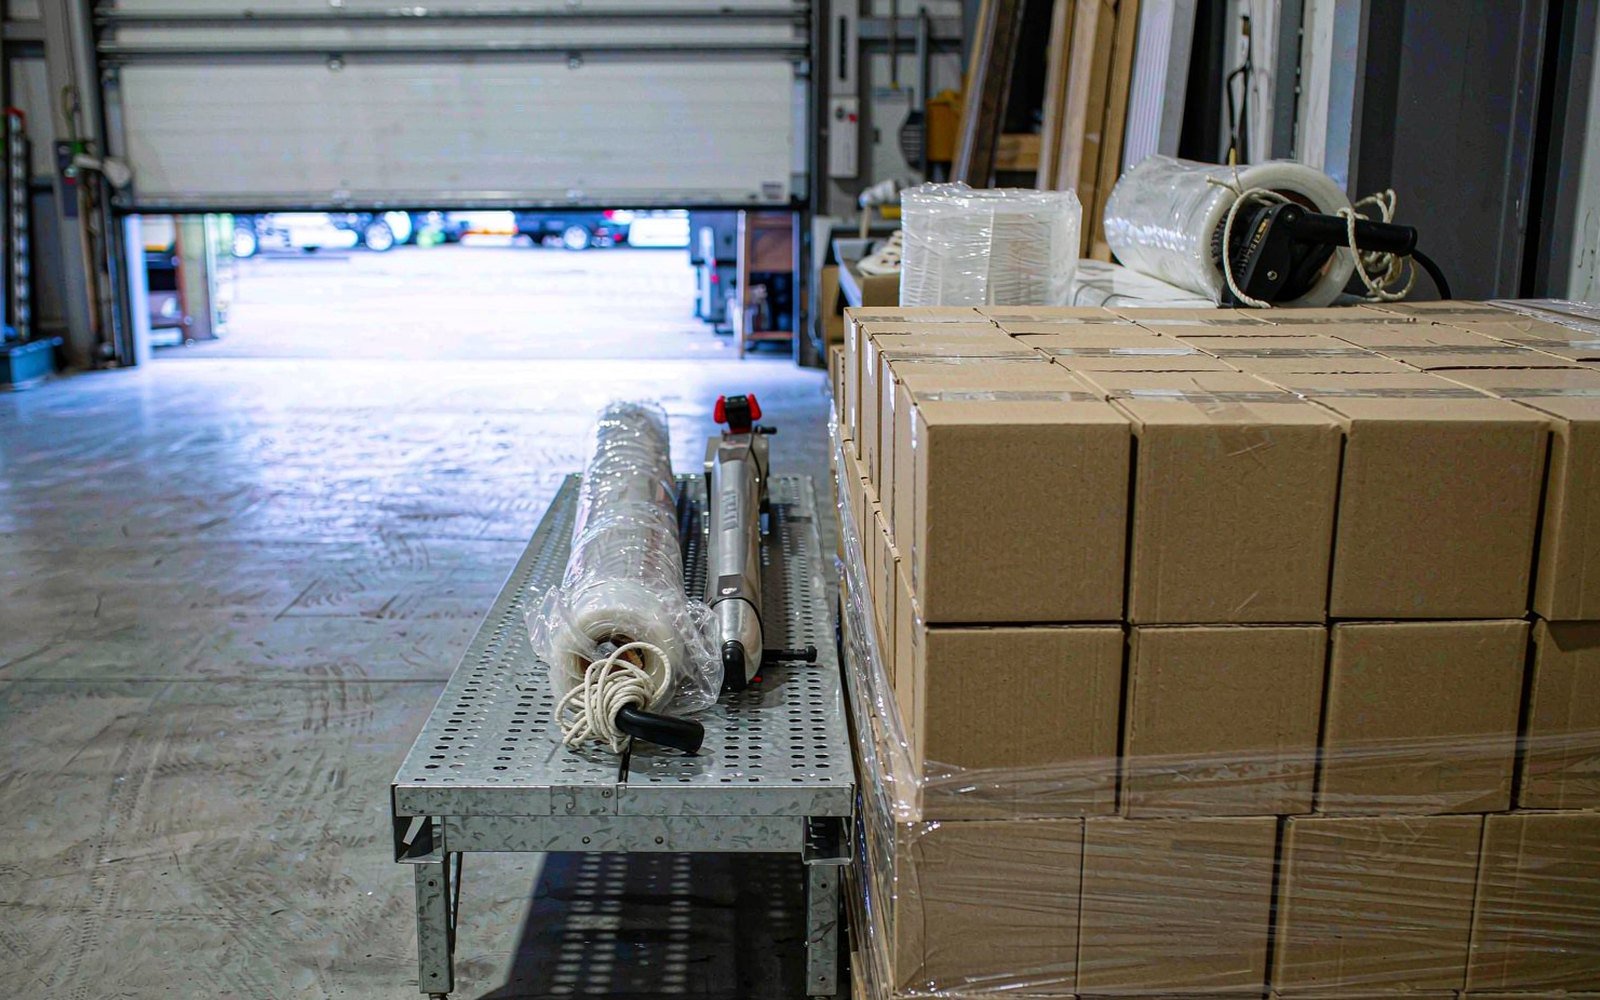
| Final assembly & packing | Product is assembled, checked, bagged and packed to the agreed packing method. | Retail-ready or bulk export — the same team packs both, so the carton is decided with the product, not after it. |
What the specification actually controls.
Most of the difference between a “garden” item and a “club” item sits in four decisions. All four are made in writing before the run starts.
Steel tube & section
Diameter, wall thickness and section are specified per product. Heavier wall and larger section are how a frame is built for daily club use rather than occasional home use.
Powder coat
Colour to RAL or to your sample, matte or satin. Coating is applied after welding and drilling, so every hole is coated and no bare edge is left exposed.
Net grade & mesh
Twine thickness, mesh size and knot type are chosen against the ball, the impact and the expected service life — the single biggest lever on how a rebounder feels.
Moulded parts
Caps, feet, joints and target panels are moulded in house. That is what keeps a replacement foot or a spare joint available instead of obsolete.
Four points where a frame gets stopped.
Inspection is built into the route rather than added at the end, because a bent frame found after coating has already cost the coating.
Incoming material
Tube, netting and moulded parts are checked against the specification on arrival — section, wall, mesh and colour lot.
Frame, before coating
Dimensions, square, weld quality, hole positions and deburring are checked while the frame is still bare steel.
Coating & net
Coating coverage and colour are checked after curing; net tension, binding and attachment are checked on the assembled item.
Packing & carton
Quantity, packing method and carton marking are checked before the carton is sealed, and again on the loaded pallet.
Want the checks written into the order? Inspection points and the sample that sets the standard can be named in the specification and on the invoice.
Ask for a specificationPacked for the channel it is sold in.
The same product leaves in very different cartons depending on where it is going, and getting that wrong is expensive on both ends: a retail box that arrives crushed, or a plain carton that cannot go on a shelf.
Packing method is confirmed with the quotation, not afterwards. Options include poly bag, carry bag, colour box, and plain export carton, with carton marking to your format and barcodes if your channel needs them.
- Carton dimensions and gross weight recorded per item on the packing list
- Carton marking and shipping marks to the buyer’s format
- Export documents issued with the shipment: invoice, packing list, and the transport document for the agreed term
- Certificate of origin and any market-specific document quoted per destination
We do not publish plant size, headcount or output.
Those numbers are easy to print and hard to keep honest, and they rarely answer the question a buyer is actually asking. What matters is whether a specific frame, in a specific quantity, can be built to a specific date at a specific price.
So we answer that instead. Send the item, the quantity and the destination port, and the reply is written against your project rather than against an average.
Tell us the item, the quantity and the port.
We will come back with the applicable specification, the price against that quantity and a realistic production window — in writing, before any tooling is discussed.
Sophia Liu, Sales Manager · Sophia@csxsports.com · WhatsApp +86 159 2704 3453